 简体中文
 English

How to Determine Whether the Iron Discharge Performance of a Permanent Magnetic Drum Separator Meets Standards?
release time:
2025-03-03
During the operation of a permanent magnetic drum separator, a layer of iron powder always remains on the drum surface and cannot be fully discharged. As the drum rotates back to the separation zone, this residual iron p
During operation of the permanent magnetic drum separator, a layer of iron powder always remains on the drum surface and cannot be fully discharged. As the drum rotates back to the separation zone, this residual iron powder is carried into the concentrate, greatly reducing the iron removal effect. Many customers assume the magnetic force is insufficient, but the problem usually lies in the iron discharge stage.
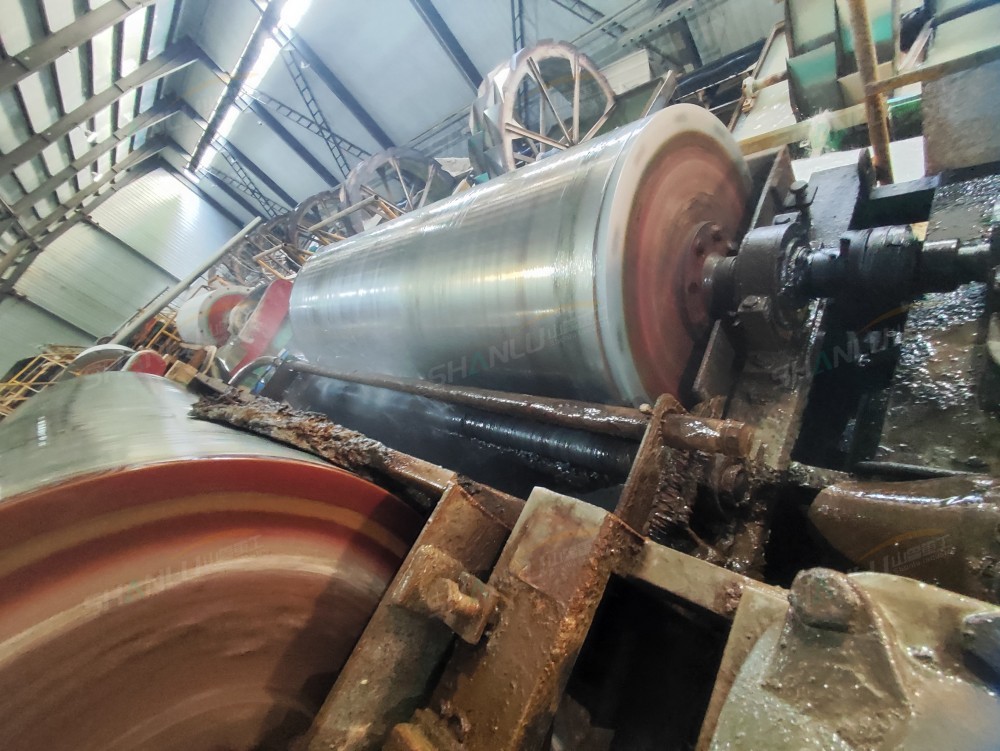
Worn or excessively gapped discharge scraper is the most common cause. The gap between the scraper and the drum surface should generally be controlled at 0.5-1mm. If the gap is too large, iron powder cannot be scraped clean and remains on the drum; if the gap is too small, the scraper and drum rub hard against each other, accelerating wear on both. It is recommended to check scraper wear every two weeks and replace it when wear exceeds one-third of the original thickness. When installing a new scraper, use a feeler gauge to calibrate the gap and keep it uniform along the entire length of the drum.
Material sticking to the drum surface will aggravate iron discharge difficulty. When material moisture content is high or there is too much fine powder, the fine powder adheres to the drum surface and forms a thin shell, causing iron powder to stick to the shell and resist scraping off. The feed moisture content should be controlled below 1%, and a hot air drying device should be installed before dry magnetic separation. After each shift shutdown, clean the drum surface with a wire brush to keep it smooth.
Improper design of the magnetic system wrap angle means the magnetic field in the iron discharge zone is not fully demagnetized. The magnetic system wrap angle determines the distribution of the separation zone and the iron discharge zone. If there is still a certain magnetic field strength in the iron discharge zone, the iron powder is held by magnetic force and cannot be scraped clean by the scraper. A gaussmeter can be used to measure the magnetic field strength on the drum surface in the iron discharge zone, which should normally be close to zero. If it is obviously too high, contact the manufacturer to adjust the magnetic system wrap angle or replace the magnetic system.
During daily inspections, pay attention to whether the iron powder discharged from the iron discharge port is continuous and clean. If residual iron powder is found on the drum surface, first adjust the scraper gap, then check for material sticking to the drum, and finally inspect the magnetic system. For equipment operation-related issues, you are welcome to call Shanlu Heavy Industry: Manager Zhang 13583776655 (same on WeChat).
related news


E-mail:
Hotline:
cell phone:
Copyright © 2012-2026 Shandong Shanlu Heavy Industry Technology Co., LTD All rights reserved 备案号:鲁ICP备2020040039号
